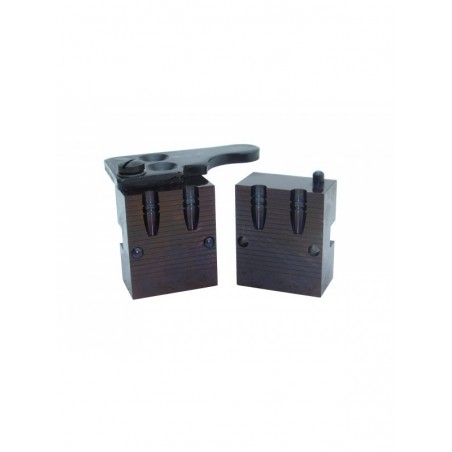

LEE Single-Cavity Mold specifically engineered for the .338 caliber, designed to produce precision projectiles with exceptional consistency and reliability.
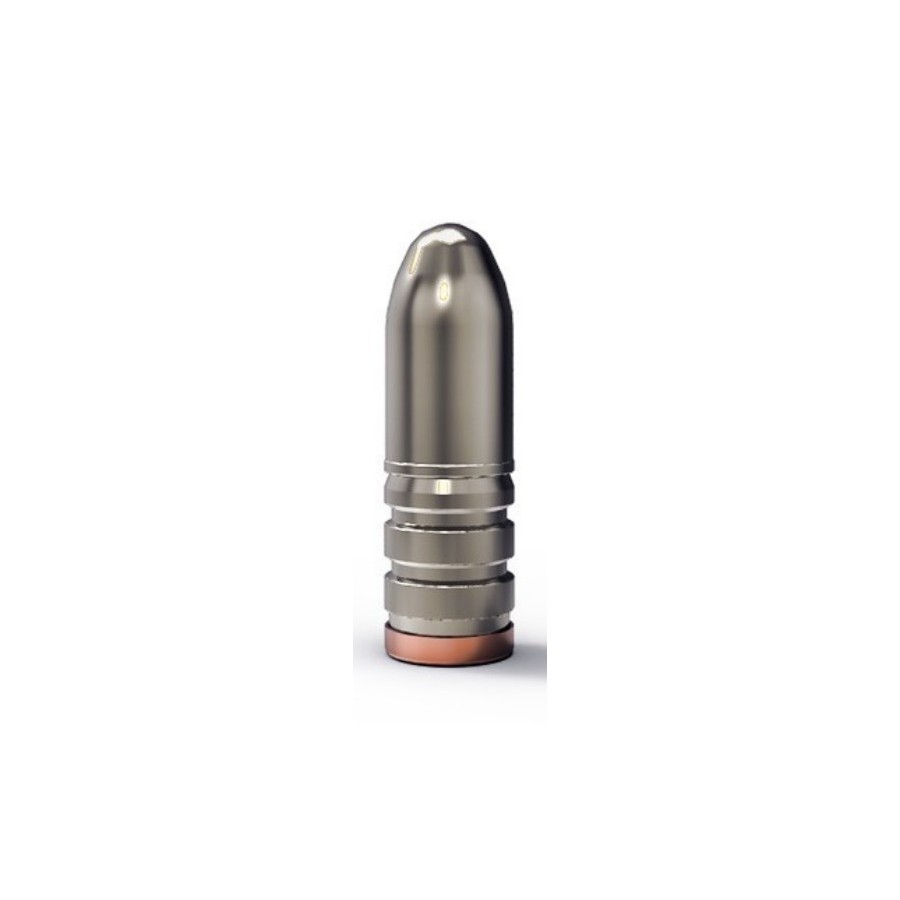
This mold casts bullets with a diameter of .338 inches and a weight of approximately 220 grains, optimized for use with Gas-Chek® style gas seals, tailored for the .338 Winchester Magnum cartridge platform.
Featuring a ballistic coefficient of approximately 0.250, these bullets offer enhanced aerodynamic efficiency, contributing to superior downrange performance and accuracy in both hunting and long-range shooting applications.
LEEs single-cavity molds are highly regarded among metallic and semi-metallic reloaders seeking a durable, cost-effective solution without compromising on quality or precision.
Constructed from high-grade aluminum blocks, these molds exhibit excellent corrosion resistance, ensuring longevity and consistent bullet dimensions over extensive casting sessions.
Aluminum molds offer thermal advantages over traditional iron or steel molds, cooling and heating more rapidly, which facilitates faster casting cycles and improved bullet surface finish.
Additionally, the lightweight nature of aluminumapproximately one-third the weight of iron or steel moldsreduces operator fatigue during prolonged bullet production, enhancing user comfort and efficiency.
The mold halves are securely clamped by robust wooden-handled tongs, preventing any lateral or vertical movement during the casting process, thereby maintaining dimensional accuracy and preventing defects.
Bullet weights may vary slightly depending on the specific lead alloy composition used, allowing reloaders to fine-tune their loads according to ballistic requirements.
Included with the mold are high-quality tongs featuring ergonomic wooden grips for safe and comfortable handling during high-temperature casting operations.
An integrated, precision-machined sprue cutter facilitates clean separation of molten lead from the bullet cavity, ensuring smooth, uniform projectiles with minimal post-cast finishing.
Prior to initial use, it is strongly recommended to thoroughly degrease the mold to remove any manufacturing residues. Subsequent seasoning with smoke or application of specialized mold treatment products enhances bullet release and extends mold life.
It is critical to never lubricate the interior cavity of the mold, as this can adversely affect bullet surface quality and dimensional consistency.
Light lubrication of the sprue cutter retaining screw is advised to maintain smooth operation and prevent seizing during repetitive casting cycles.
LEE Single-Cavity Mold specifically engineered for the .338 caliber, designed to produce precision projectiles with exceptional consistency and reliability.
This mold casts bullets with a diameter of .338 inches and a weight of approximately 220 grains, optimized for use with Gas-Chek® style gas seals, tailored for the .338 Winchester Magnum cartridge platform.
Featuring a ballistic coefficient of approximately 0.250, these bullets offer enhanced aerodynamic efficiency, contributing to superior downrange performance and accuracy in both hunting and long-range shooting applications.
LEEs single-cavity molds are highly regarded among metallic and semi-metallic reloaders seeking a durable, cost-effective solution without compromising on quality or precision.
Constructed from high-grade aluminum blocks, these molds exhibit excellent corrosion resistance, ensuring longevity and consistent bullet dimensions over extensive casting sessions.
Aluminum molds offer thermal advantages over traditional iron or steel molds, cooling and heating more rapidly, which facilitates faster casting cycles and improved bullet surface finish.
Additionally, the lightweight nature of aluminumapproximately one-third the weight of iron or steel moldsreduces operator fatigue during prolonged bullet production, enhancing user comfort and efficiency.
The mold halves are securely clamped by robust wooden-handled tongs, preventing any lateral or vertical movement during the casting process, thereby maintaining dimensional accuracy and preventing defects.
Bullet weights may vary slightly depending on the specific lead alloy composition used, allowing reloaders to fine-tune their loads according to ballistic requirements.
Included with the mold are high-quality tongs featuring ergonomic wooden grips for safe and comfortable handling during high-temperature casting operations.
An integrated, precision-machined sprue cutter facilitates clean separation of molten lead from the bullet cavity, ensuring smooth, uniform projectiles with minimal post-cast finishing.
Prior to initial use, it is strongly recommended to thoroughly degrease the mold to remove any manufacturing residues. Subsequent seasoning with smoke or application of specialized mold treatment products enhances bullet release and extends mold life.
It is critical to never lubricate the interior cavity of the mold, as this can adversely affect bullet surface quality and dimensional consistency.
Light lubrication of the sprue cutter retaining screw is advised to maintain smooth operation and prevent seizing during repetitive casting cycles.